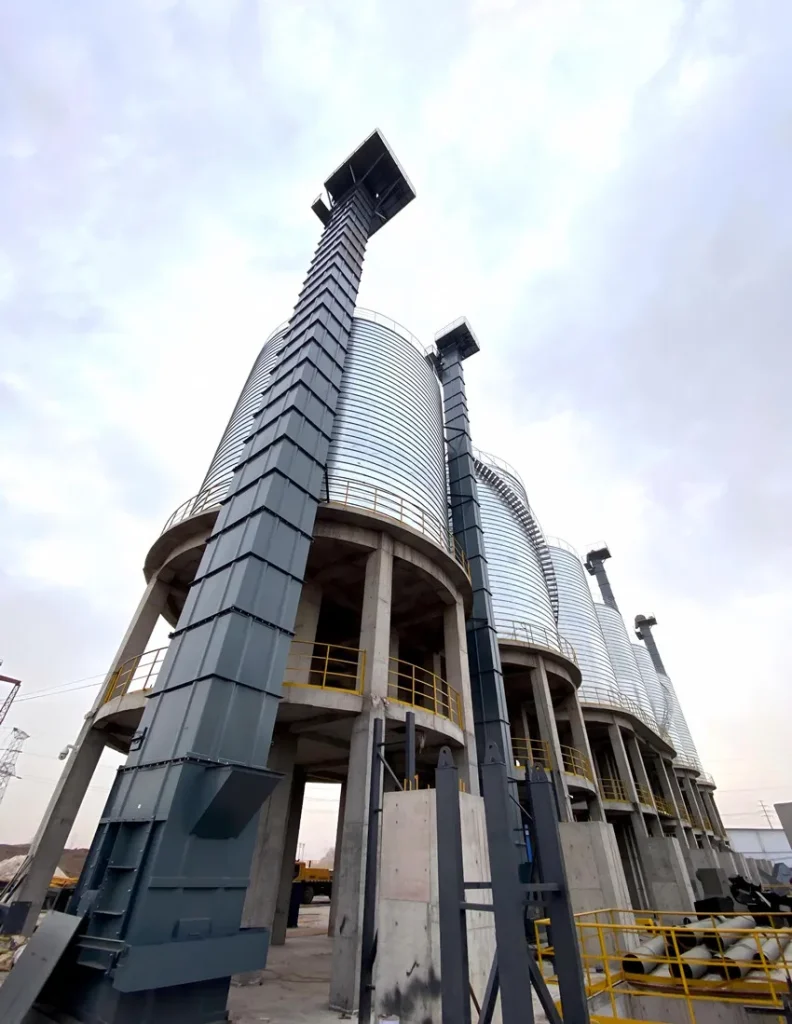
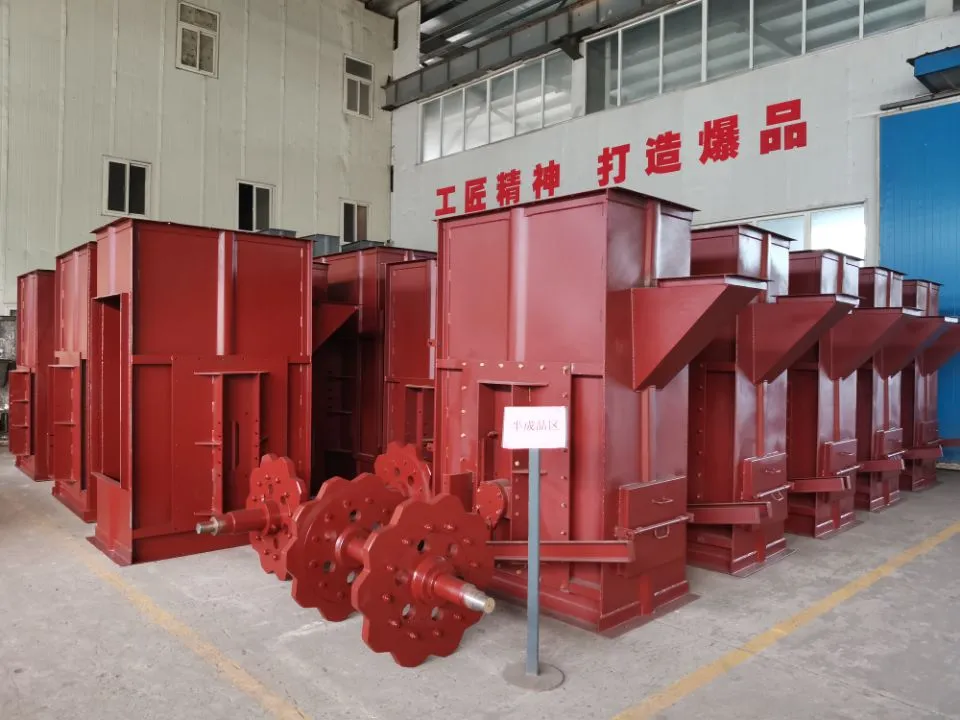
As a bucket elevator manufacturer with 30 years of production experience, we have developed three main categories of bucket elevators – Plate-Chain, Belt, and Chain (Circular-Link) Type – to meet the diverse needs of various industries. They are widely used in power plants, building materials, metallurgy, chemical industries, and more. Below is a detailed introduction to the characteristics, suitable materials, and industry applications of each model.
I. Plate-Chain Bucket Elevator
Characteristics
High-Strength Wear-Resistant Plate Chain: Uses alloy steel forged chains, resistant to high temperatures and impact, suitable for large, sharp materials.
Large-Capacity Buckets: Deep or scale-type bucket design offers large loading capacity and high conveying efficiency.
Stable and Reliable: Ideal for high lifts exceeding 50 meters, operates smoothly with low failure rates.
Suitable Materials: Large-particle, high-temperature (≤250°C) materials such as ore, cement clinker, limestone, coke, sintered ore.
Application Fields: Metallurgical industry (blast furnace raw material conveying), Building materials industry (cement plants, sand & aggregate), Chemical industry (fertilizers, slag).
II. Belt-Type Bucket Elevator – Efficient Conveying for Lightweight & Powdery Materials
Characteristics:
Rubber Belt Traction: Smooth operation, low noise, suitable for lightweight, fragile materials.
Anti-Deviation Design: Features automatic deviation correction devices, reducing maintenance costs.
Economical: Low energy consumption, suitable for continuous conveying of small-particle or powdery materials.
Suitable Materials: Powdery or small-particle materials such as coal dust, grain, fertilizer, plastic pellets, feed.
Application Fields: Power industry (coal conveying in coal-fired power plants), Food industry (flour, grain lifting), Chemical industry (plastic pellets, lightweight powders).
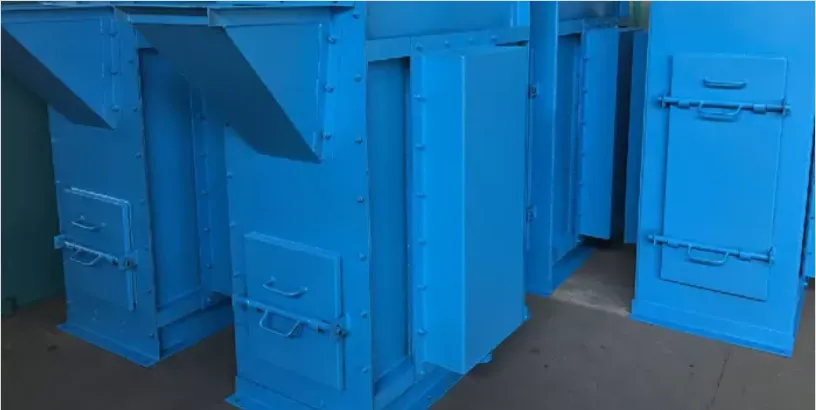
III. Chain (Circular-Link) Bucket Elevator – Medium/Long Distance, High Wear Resistance
Characteristics:
Forged Alloy Steel Chain: High tensile strength, excellent wear resistance, long service life.
Modular Design: Easy maintenance and quick replacement of wear parts.
Strong Adaptability: Suitable for medium-distance to long-distance conveying (30-80 meters) of medium-density materials.
Suitable Materials: Medium-density, non-high-temperature materials such as coal, fertilizer, mineral powder, cement raw meal.
Application Fields: Coal industry (coal washing plants, coking plants), Building materials industry (raw material conveying in cement plants), Chemical industry (fertilizer, chemical raw materials).
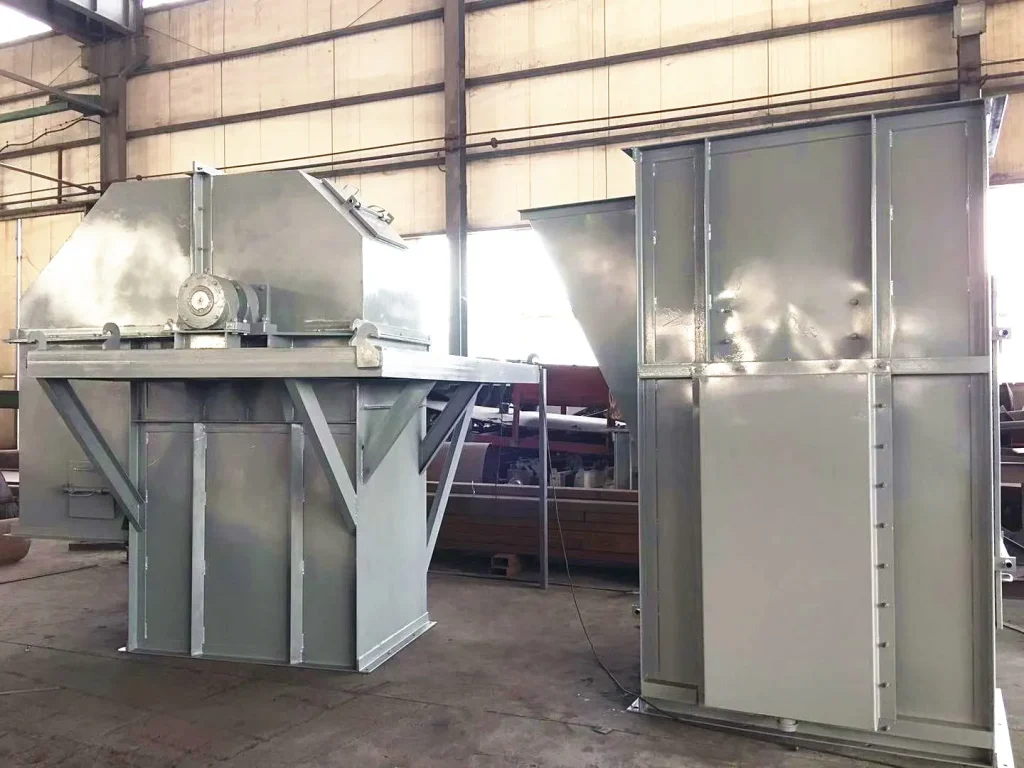
Based on the specific characteristics of different industries, we provide customized bucket elevator solutions to ensure stable, durable, and low-maintenance equipment. Whether it’s conveying heavy lump materials, powdery substances, or medium/long-distance lifting, we can provide the bucket elevator right for your needs.